Why Choose a PE Strapping Machine for Global Packaging?
Why Choose a Pe Strapping Machine for Global Packaging?
Global packaging demands more than speed. It requires stable performance across different climates, products, operators, and shipping routes. A PE Strapping Machine can secure cartons, pallet loads, and grouped products with consistent tension. It also reduces repetitive manual work on busy production floors.
Packaging systems expert Dr. Susan Selke has said, “Packaging is a system, not just a container.” This principle matters when selecting a strapping solution. The machine must match the product, conveyor layout, strap width, sealing method, and expected daily volume. A lightweight PE strap can protect many loads without adding unnecessary weight. It can also reduce material use when tension is properly controlled.
Small details matter. A loose strap may shift during sea transport. Excessive tension may crush a carton’s edges. Humidity can affect storage conditions, while voltage differences can complicate installation. Reliable machines should offer adjustable tension, repeatable heat sealing, accessible controls, and straightforward maintenance. Operators should not need advanced technical skills for every adjustment.
The decision is not flawless. A PE Strapping Machine may cost more than manual tools at the beginning. It also needs training, spare parts, and suitable integration. Those limits deserve honest attention. Still, verified throughput, lower labor strain, and consistent load stability can improve long-term value.
Real performance should be tested. Measure cycle time. Check seal strength. Inspect damaged corners. Compare results across different carton sizes and shipping conditions. A practical evaluation often reveals more than a sales brochure.
PE Strapping Basics: 5–19 mm Widths and 0.4–1.0 mm Gauges
Why Choose a PE Strapping Machine for Global Packaging?
PE Strapping Basics: 5–19 mm Widths and 0.4–1.0 mm Gauges
Polyethylene (PE) strapping supports cartons, bundled pipes, and palletized goods during handling. Its practical range covers widths from 5 to 19 mm and gauges from 0.4 to 1.0 mm. Narrow 5–9 mm straps suit light cartons and small bundles. Wider straps provide better load distribution for heavier packages. That detail matters.
Gauge affects stiffness, elongation, and resistance to tearing. A 0.4 mm strap may work well for stable, lightweight boxes. A 1.0 mm option offers more material strength for dense loads. However, thicker is not always better. It can increase material use and require stronger machine tension. In field testing, poor alignment often causes failures before strap strength does.
A PE strapping machine should match the selected width and gauge precisely. Guides, sealing temperature, feed speed, and tension need careful adjustment. Operators should test several packed loads, not only an empty carton. Measure twice. Check strap edges after sealing. Sharp creases may signal excessive tension or unsuitable settings. Packaging conditions also change across regions. Cold storage can reduce flexibility, while heat may affect seal performance. The neatest specification sheet cannot replace a practical trial. Not always.
PE Strapping Linear Mass by Width and Gauge
This chart shows the calculated linear mass of PE strapping across common widths from 5 to 19 mm and gauges from 0.4 to 1.0 mm. Values are based on a PE density of 0.94 g/cm³ using the formula: linear mass = width × gauge × density.
Heat-Seal Performance: 30–60 Straps per Minute in Automated Lines
Why Choose a PE Strapping Machine for Global Packaging?
Heat sealing changes the rhythm of an automated packaging line. A well-tuned PE strapping machine can apply 30–60 straps per minute, depending on package size, tension, and conveyor spacing. That equals one strap every one or two seconds. Fast, but not effortless.
The heat-sealing head softens overlapping PE strap surfaces and creates a compact joint without metal clips. This reduces loose ends around cartons, pallets, and bundled products. Operators should still verify seal strength, because excessive heat can deform the strap. Too little heat can produce a weak joint. Small mistakes become expensive at scale.
According to PMMI’s 2024 State of the Industry report, labor availability and equipment uptime remain major packaging investment concerns. Automated strapping addresses both, while consistent tension helps reduce material variation. Smithers’ The Future of Packaging to 2028 report also projects continued global packaging growth, increasing pressure on flexible, high-throughput systems. However, the advertised 30–60 straps per minute should not be treated as a guaranteed production rate. Product geometry, PE grade, cooling time, and line integration may lower actual output. Test the complete line first. That part is often overlooked. Experiences from commissioning trials show that stable feeding and accurate sensor timing matter as much as sealing temperature. Reliable performance comes from measured settings, routine inspection, and documented seal tests.
ASTM D3950: Matching Strap Tensile Strength to Packaging Loads
Why Choose a PE Strapping Machine for Global Packaging?
ASTM D3950 provides a useful framework for evaluating nonmetallic packaging strap performance. It helps teams compare tensile strength, elongation, dimensions, and joint quality. These properties must match the packaging load, not merely the machine setting. A light carton may need moderate tension and flexible PE strap. A dense pallet needs stronger resistance against shifting and impact.
Tensile strength is only one part of the decision. Measure the load during lifting, stacking, vibration, and sudden braking. Then select strap strength with a practical safety margin. Do not confuse machine tension with strap strength. The machine applies force; the strap carries it. Heat, moisture, sharp edges, and long-distance handling can reduce real-world performance.
Small details matter.
During packaging trials, operators should inspect strap stretching, seal stability, and corner damage. A strap that looks secure may loosen after several days in storage. Edge protectors can reduce cutting at carton corners. Correct tension also prevents crushed boxes and unstable loads. ASTM D3950 supports consistent testing, but laboratory results cannot represent every route. A trial pallet is still necessary. It may reveal an uncomfortable mistake in the original calculation. For global shipments, record strap specifications, test results, machine settings, and inspection findings. This creates a reliable process that can be reviewed when packaging conditions change.
Why Choose a PE Strapping Machine for Global Packaging? - ASTM D3950: Matching Strap Tensile Strength to Packaging Loads
The examples below use a 1.5 dynamic-load factor, a 2.0 design safety factor, and an assumed 70% effective joint efficiency. Actual strap selection should be confirmed through certified ASTM D3950 test data, package geometry, transport conditions, and machine sealing performance.
| Packaging Scenario | Package Mass
(kg) | Recommended
Straps | Design Load per Strap
(N) | Minimum Certified Strap Strength
(N / kgf) | PE Strap Suitability | Packaging Application |
| Light cartons and small bundles | 50 | 2 | 736 | 1,051 / 107 | Generally suitable when certified strength is met | Retail cartons, printed boxes, light parcel consolidation |
| Medium carton assemblies | 100 | 2 | 1,471 | 2,101 / 214 | Suitable only with verified strap and joint performance | Grouped cartons, appliance packaging, export bundles |
| Heavy cartons or compact loads | 250 | 2 | 3,677 | 5,252 / 536 | Use only after load testing confirms PE performance | Dense cartons, spare-part containers, compact export cases |
| Palletized medium-duty goods | 500 | 4 | 3,677 | 5,252 / 536 | Borderline for PE; verify creep and joint retention | Palletized cartons, light industrial components, warehouse transfers |
| Large palletized loads | 750 | 4 | 5,516 | 7,880 / 804 | Usually unsuitable unless a high-strength PE system is validated | Heavy pallet loads requiring high retention during road or sea transport |
| Very heavy or high-risk loads | 1,000 | 6 | 4,903 | 7,004 / 714 | Not recommended without documented engineering validation | Heavy machinery, dense construction materials, high-consequence shipments |
Calculation basis: Design load per strap = package mass × 9.80665 m/s² × 1.5 dynamic factor × 2.0 safety factor ÷ number of straps. Minimum certified strap strength = design load per strap ÷ 0.70 assumed joint efficiency. ASTM D3950 should be used together with the applicable strap specification, dimensional requirements, tensile test results, elongation data, and joint-strength verification.
Global Integration: 400–1,200 mm Conveyor Heights and Safety Controls
Why Choose a PE Strapping Machine for Global Packaging?
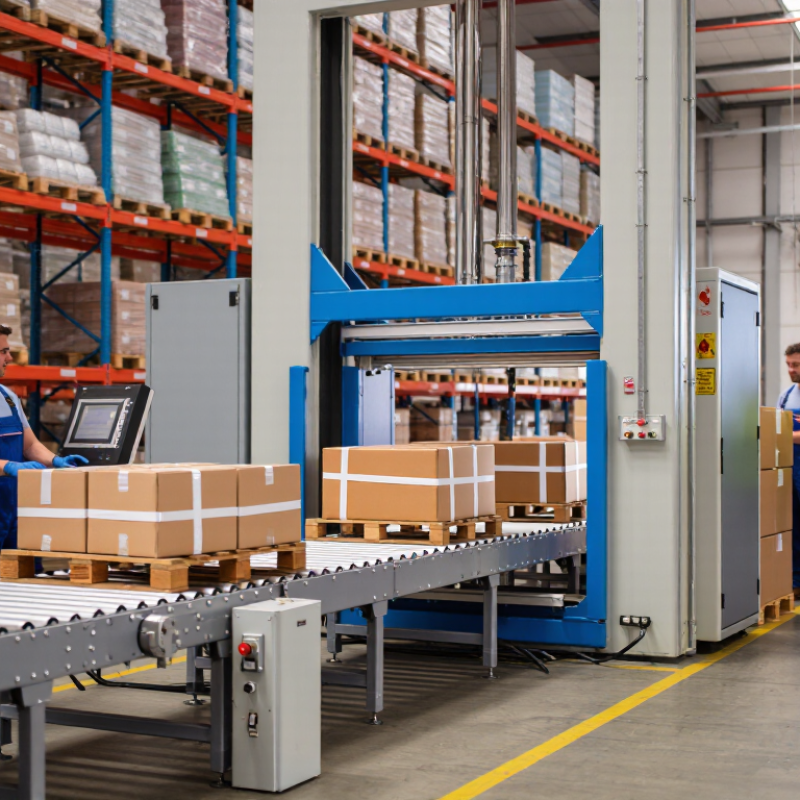
A PE strapping machine supports consistent carton securing across varied production environments. Its 400–1,200 mm conveyor-height range suits floor-level packing, standard workstations, and elevated lines. This flexibility matters when operators, cartons, and pallet patterns change between facilities. In practice, a 400 mm setup can reduce transfer distance for heavy boxes. At 1,200 mm, it can align with automated conveyors and inspection equipment.
Safety controls should travel with that flexibility. Guarded strap paths, emergency stops, access interlocks, and photoelectric sensors help prevent contact with moving parts. Controls should also support clear fault messages and lockout procedures. ISO 12100 and ISO 13849-1 provide useful frameworks for risk assessment and safety-related control design. MHI’s 2024 Annual Industry Report found that 55% of respondents considered supply-chain innovation very or extremely important. Integration is no longer optional for many sites.
PE strapping also offers stable tension and repeatable sealing when operators follow correct settings. The machine still needs careful commissioning. A conveyor height range alone cannot solve poor ergonomics or uneven floors. I have seen efficient lines lose time because sensor positions were adjusted too late. That detail is easy to overlook. Independent validation, operator training, and documented maintenance records strengthen reliability across global facilities.
 Skip to content